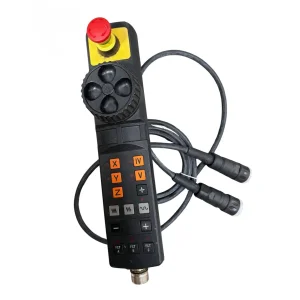
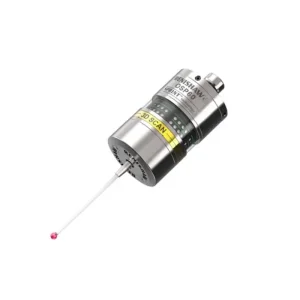
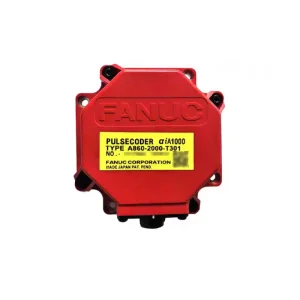
Featured OEM precision probes, stylus systems, and high-frequency encoders optimized for immediate export and industrial integration in Montevideo, Canelones, and Salto.
An in-depth analysis of Uruguay’s growing advanced manufacturing sectors and the strategic role of automated CNC metrology.
Uruguay’s industrial sector is undergoing a rapid technological transformation. Driven by high-value niche manufacturing, agro-industrial equipment production, pulp and paper mega-complexes (such as UPM and Montes del Plata), and a burgeoning automotive component sector in San José and Montevideo, Uruguayan machine shops are shifting toward high-precision automated machining.
Unlike massive low-cost commodity production hubs, Uruguay's manufacturing competitiveness hinges on extreme accuracy, process repeatability, and minimal operational downtime. To achieve these metrics, CNC machine tools across the country—ranging from 5-axis vertical machining centers to heavy-duty horizontal boring mills—require state-of-the-art metrology feedback hardware.
Key Insight: In Uruguay’s humid subtropical climate (Cfa), thermal variation in machine tool structures can introduce dimensional drift up to 35 µm over an 8-hour shift. Automated tool setting and workpiece probing using high-rigidity Renishaw components reduce scrap rates by up to 88% in local mold & die facilities.
Modern machine shops in Montevideo Free Zone (Zona Franca) and surrounding industrial corridors require immediate access to original replacement spare parts to support continuous 24/7 operations.
Understanding kinematic resistive mechanisms, thermal coefficient matching, and signal transmission integrity for Uruguayan machine setups.
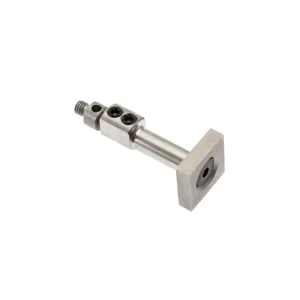
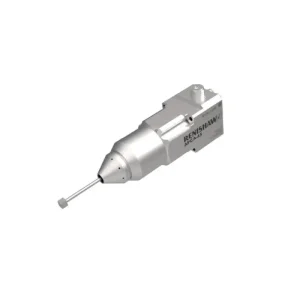
Renishaw's dominance in machine tool metrology is rooted in fundamental mechanical and optical engineering precision. When selecting spare parts—such as the M4 Tungsten Steel Datuming Cube Stylus (A-2197-0160) or the OSP60 Optical Scanning Probe—engineers must consider physical kinematics, deflection dynamics, and interface protocols.
| Metrology Component | Core Technical Parameter | Kinematic / Operational Spec | Industrial Application in Uruguay |
|---|---|---|---|
| M4 Cube Stylus (A-2197-0160) | 34.5 mm length, Tungsten Carbide stem | Concentricity < 0.5 µm, Zero thermal hysterisis | Tool setting & broken tool detection on CNC lathes |
| OSP60 Scanning Probe | 3D optical transmission / Sprint™ tech | 1,000 data points/sec, 0.25 µm 2D repeatability | High-speed freeform surface measurement (Molds) |
| APC / APCA / APCS-45 | Contact Tool Setter with pneumatic arm | Sub-micron repeatability, IP68 sealed housing | Automated CNC machining centers with heavy coolant spray |
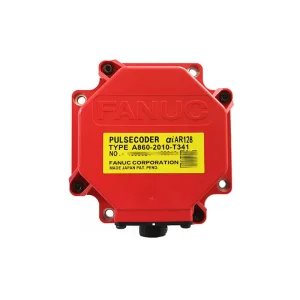
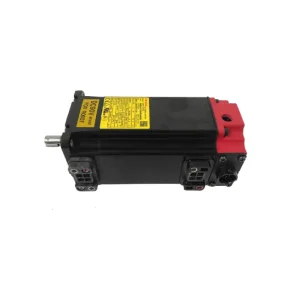
| Fanuc A860 Encoders | 128 ALPHA i-A high-resolution feedback | Serial optical interface, 1,000,000 ppr resolution | Closed-loop spindle & axis positioning accuracy |
Standard touch-trigger probes rely on a precision three-point kinematic seating arrangement: three equally spaced steel rods resting on six tungsten carbide balls. When the stylus deflects upon touching a workpiece, the electrical resistance through the contact points changes, triggering a latch signal to the CNC controller (FANUC 0i-MF, Siemens SINUMERIK 828D, or Mitsubishi M80).
For high-speed contouring and scanning in Uruguayan defense or aerospace workshops, scanning probes like the Renishaw OSP60 utilize strain gauge sensors integrated into the probe body. This decouples trigger sensitivity from stylus length and mass, allowing long stem extensions (up to 150 mm) without compromising sub-micron repeatability.
Tungsten carbide stems offer exceptional bending stiffness, essential for short-to-medium styli lengths (34.5 mm). They minimize pre-travel variation under contact force, guaranteeing precise tool offsets.
Optical infrared interfaces (OMP/OSP) utilize modulated optical transmission algorithms to prevent line-of-sight signal degradation caused by heavy emulsion coolants or metal swarf in high-chip-load turning.
Industrial tool setters (APCA-45) feature fluoroelastomer seals and metallic bellows designed to withstand aggressive synthetic cutting fluids and abrasive cast-iron dust common in Uruguayan foundries.
Why procurement managers in Montevideo, Salto, and Paysandú source genuine Renishaw and CNC spare parts through specialized Chinese manufacturing & stockist networks.
Traditionally, Uruguayan machine shops sourcing European precision components faced lead times of 8 to 12 weeks, accompanied by exorbitant regional distributor markups. This extended downtime severely affected plant productivity and increased total cost of ownership (TCO).
By leveraging specialized Ningbo/Shanghai export hubs, industrial buyers in Uruguay gain direct access to extensive, verified stocks of 100% brand-new, original components. Orders leave Chinese warehouses within 24 to 72 hours, arriving via air express at Carrasco International Airport (MVD) in as few as 5 to 7 days.
Importing machinery parts into Uruguay requires compliance with National Customs Directorate (Dirección Nacional de Aduanas) regulations, LATU certifications, and Mercosur Common External Tariff (AEC) guidelines.
Established Chinese supply partners provide comprehensive documentation, including detailed HS Code classifications (e.g., HS 9031.90 for metrology parts, HS 8537.10 for CNC drives), original manufacturer serial numbers, and custom origin declarations, ensuring seamless customs clearance at the Port of Montevideo.
Real-world implementations of automated tool setting and encoder feedback systems across key Uruguayan industrial operations.
Problem: A prominent plastics injection mold maker in the Paso de la Arena industrial district suffered frequent tool breakage during unmanned overnight milling of hardened tool steel (HRC 54+). Tool wear went undetected, causing multi-thousand-dollar mold core damage.
Solution: Retrofitting the 3-axis CNC vertical machining center with a Renishaw APCA-45 Contact Tool Setter paired with an M4 Tungsten Steel Datuming Cube Stylus (A-2197-0160).
Result: Automated Z-axis length offsets and broken tool checks executed every 15 minutes. Tool setting time dropped from 12 minutes to 18 seconds, eliminating scrap and adding $45,000 annually in plant capacity.
Problem: A agricultural equipment gearbox builder experienced spindle positioning errors and encoder alarm codes on their Fanuc-controlled heavy CNC lathe during peak harvest repair seasons.
Solution: Direct replacement of the compromised spindle sensor head with an original Fanuc Sensor Head Encoder A860-2162-V001 and replacement pulse encoders dispatched via overnight air freight.
Result: Full C-axis orientation and threading sync restored within 48 hours of dispatch, preventing weeks of agricultural field delays during the critical soybean harvesting period.
How smart sensors, closed-loop probing, and high-speed digital feedback drive operational resilience.
The Latin American manufacturing paradigm is rapidly evolving from manual setup to fully integrated, closed-loop automated manufacturing. In Uruguay, where skilled CNC machinist labor commands premium wages, implementing automated in-process measurement is a strategic imperative.
By feeding real-time inspection data from Renishaw OSP60 probes directly into CNC controllers (Siemens 828D / Fanuc 0i-F), the machine automatically updates tool wear offsets without operator intervention, achieving true zero-defect machining.
Modern feedback devices, including Fanuc ALPHA i-A encoders and Siemens SIMOTICS servo motors, transmit real-time telemetry (vibration, thermal load, optical degradation) to controller diagnostics, preventing unexpected total breakdown.
Instead of investing hundreds of thousands of dollars in new machine tools, Uruguayan workshops retrofit existing Japanese and European CNC lathes with Heidenhain HR410 handwheels and modern touch probes, extending machine service life by 15+ years.
Step-by-step guidance for procurement officers and plant engineers ordering industrial spare parts from international stockists.
CNC control electronics, servo drives, and probing systems have complex order matrix codes. A single character difference in a Fanuc motor part number (e.g., A06B-0116-B855#0059) can signify a different shaft keyway, brake type, or encoder communication protocol.
Our senior metrology engineers and CNC hardware specialists are ready to cross-reference your part numbers and provide immediate price and delivery quotes for Uruguay.
Send Inquiry Now (Fast 24h Response)Authoritative technical answers to common queries from Uruguayan engineers, CNC maintenance teams, and procurement managers.
Comprehensive spare parts inventory supporting FANUC, Siemens, Mitsubishi, Delta, and Renishaw machine setups across South America.
Whether you require an immediate replacement Renishaw stylus, a Fanuc spindle encoder, or a complete Siemens servo drive upgrade, our international logistics team ensures fast, hassle-free delivery directly to your facility in Uruguay.