Precision metrology probes, digital controller units, and high-dynamics synchronous servo motors engineered for high-throughput automotive and die-mold facilities across the Salto, Itu, and Sorocaba manufacturing corridor.
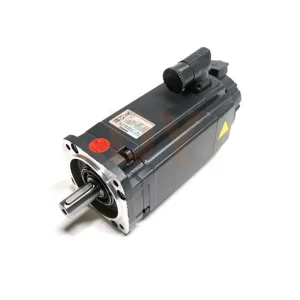
Situated in the heart of the Macrometrópole Paulista along the Tietê-Sorocaba development axis, Salto represents one of Brazil’s most vital clusters for metal-mechanics, automotive Tier-1/Tier-2 supply chains, heavy machinery fabrication, and high-precision plastic injection tooling. Neighboring the industrial powerhouses of Itu, Indaiatuba, and Campinas, manufacturing enterprises in Salto operate under stringent production metrics where line uptime determines supplier tier qualification.
With massive installations of FANUC Robodrill machining centers, 3-axis to 5-axis vertical machining systems, and heavy-duty horizontal lathes powered by FANUC 0i-MF, 0i-TF, 18i-TB, and 31i-B series controllers, local manufacturing engineers face severe challenges when dealing with legacy drive obsolescence and protracted OEM lead times.
Traditional procurement routes in the Brazilian market often quote 10 to 18 weeks for imported Japanese FANUC servo modules and optical coders. With unexpected breakdown costs in high-volume automotive stamping and engine block machining exceeding $4,500 USD per hour, waiting weeks for OEM parts is economically unsustainable.
Understanding how localized factory conditions in São Paulo state impact optical encoders, intelligent power modules (IPMs), and servo amplifier modules enables predictive intervention rather than reactive repairs.
Salto's subtropical summer temperatures combined with dense, enclosed factory enclosures accelerate electrolytic capacitor desiccation inside FANUC Alpha iSV (A06B-6114 / A06B-6117) and Beta iSV power units. Ripple current escalations lead to sudden IPM IGBT punch-through and DC bus short circuits (Alarms 401, 414, and FSSB communication drops).
High-speed milling vibrations in die and mold shops loosen pulse coder couplings. Over prolonged operational cycles, cutting oil mist and microscopic brass/graphite dust breach older labyrinth seals, contaminating the glass disk of Alpha A860-2020 and A860-2100 encoders, triggering intermittent Alarm 300, 319, or fatal pulse parity errors.
Heavy electrical loads across the industrial parks along Rodovia Santos Dumont occasionally generate harmonic distortion and voltage dips. FANUC power supply modules without upstream line filters or surge suppressors experience rectifier bridge failure and blown internal gate drive transformers under sudden re-energization.
Headquartered in Ningbo, China—the world’s foremost epicentre for CNC machine tool production, advanced precision accessory manufacturing, and electrical distribution—NINGBO DINGYAN MACHINERY CO., LTD. serves as the premier supply bridge for Latin American industry.
Rather than functioning merely as a trading portal, our facility houses comprehensive closed-loop CNC testing benches simulating authentic operational conditions for FANUC, Siemens, Mitsubishi, and Heidenhain controls. Every pulse coder, servo motor, and drive amplifier destined for international export undergoes extensive 4-hour dynamic load testing, insulation resistance evaluation, and waveform harmonics verification.
Every piece of CNC hardware leaving Ningbo for Brazil is accompanied by a dedicated Quality Inspection Certificate covering:
✔ Megger Insulation Testing (>100MΩ at 1000V DC)
✔ Optical Encoder Waveform Sine/Cosine Symmetry Analysis
✔ High-Speed Thermal Run with FSSB Optical Bus Synchronicity
✔ Customized Anti-Static, Moisture-Proof, Heavy-Duty Air Cargo Packaging
Extending machine asset longevity through systematic component-level restoration, high-precision probing retrofits, and synchronized motion automation.
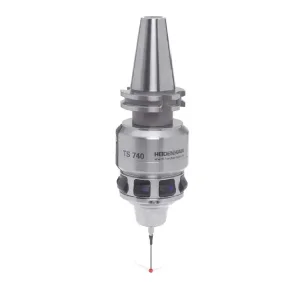
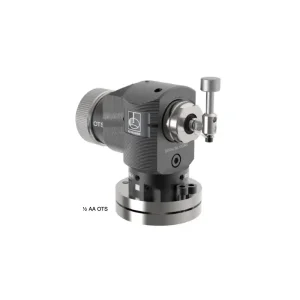
Upgrading existing Salto CNC milling centers with Renishaw (OTS, TS27R) and Heidenhain (TS740) workpiece touch probes eliminates manual edge-finding errors. Direct integration into FANUC macro subroutines (G65 P9810/P9811) reduces setup times by up to 75% and guarantees sub-5-micron tolerances on precision aerospace and powertrain castings.
When replacing high-output Alpha or Beta series spindle motors and power modules (such as A06B-0116 or equivalent high-inertia drives), specialized field-oriented vector parameter calibration is critical. DingYan assists maintenance teams with load inertia ratio calculation, velocity loop gain matching, and electronic orientation adjustments to prevent chatter marks during heavy hogging operations.
Brazilian plants frequently run hybrid shops featuring Japanese, German, and Taiwanese machining cells. DingYan eliminates the overhead of managing 8 separate vendor relationships by consolidating FANUC servo modules, Siemens SIMOTICS drives, Mitsubishi controllers, and Heidenhain feedback rulers into a unified, consolidated procurement pipeline.
Every minute of unplanned CNC stoppage incurs catastrophic financial penalties. Our four-step rapid verification and deployment cycle guarantees first-time mechanical and electrical fit.
Submit a high-resolution nameplate photograph. Our technical team checks exact suffix designations, shaft tapers, keyways, feedback interface types (serial pulse coder vs. resolver), and rated voltage.
The unit is retrieved from our Ningbo inventory and mounted on a dedicated OEM test bench. We verify optical communication, run thermal load checks, and log zero-backlash feedback readings.
Shipped in customized double-walled industrial packaging with desiccant protection. Tracking credentials and proforma customs documents with exact Mercosur NCM codes are issued within 2 hours of departure.
Our bilingual automation engineers remain on standby via WhatsApp and direct audio/video call to guide machine setup, encoder zero point datum alignment, and alarm code clearing.
Factory-original stock holding ready for prompt Latin American air shipment. Balanced multi-brand compatibility for turnkey retrofits and urgent plant maintenance.
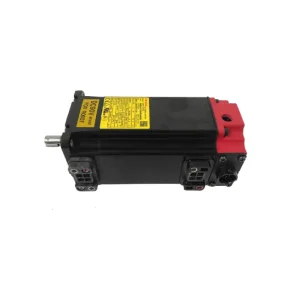
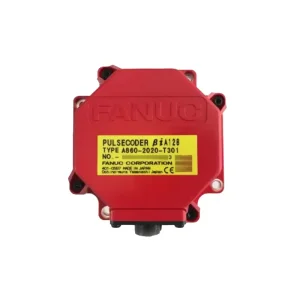
Addressing the critical commercial, import tariff, compatibility, and logistical inquiries raised by Brazilian manufacturing departments.
For urgent breakdown emergencies, we dispatch via express air priority (DHL Express, FedEx International Priority, or UPS Worldwide Saver). Shipments route into either Viracopos Cargo Terminal in Campinas (VCP) or Guarulhos International Airport (GRU) in São Paulo. Typical freight transit takes 3 to 5 business days. Once local customs clearance (Siscomex dispatch via your despachante aduaneiro or express courier broker) is finalized, road transport to Salto via Rodovia Santos Dumont takes less than 90 minutes.
Brazilian customs compliance requires meticulous documentation to avoid fiscal penalties under Receita Federal scrutiny. DingYan provides commercially compliant Proforma Invoices, Commercial Invoices, Packing Lists, and Certificates of Origin specifying exact Mercosul Common Nomenclature (NCM) codes (e.g., 8501.52 for AC servo motors, 8504.40 for static converters/drives, and 9031.80 for coordinate measuring probes). We include manufacturer part numbers and serial numbers on all paperwork to ensure frictionless import clearance.
Yes, but electrical pinouts, communication protocols, and drive widths differ. The original Alpha series communicates via Type-A or Type-B parallel interfaces, whereas Alpha i utilizes the proprietary FANUC Serial Servo Bus (FSSB) optical fiber protocol. If you are replacing an obsolete drive (e.g., A06B-6079 or A06B-6089 series), our engineers can supply either 100% factory-tested direct-replacement original units from our reserve stock or provide the specific conversion modules, optical cable adapters, and CNC parameter reconfiguration steps required to perform a modern retrofit without altering machine mechanicals.
Every single product undergoes rigorous electrical inspection at our Ningbo testing center. For FANUC servo motors and encoders, we utilize genuine FANUC 0i-F Plus CNC test racks coupled to matching Alpha i amplifier modules. The unit is run across its full RPM operating envelope, verifying pulse coder quadrant output, zero-marker pulse repeatability, brake coil holding force, and winding resistance symmetry. A digital inspection report and dynamic video verification are available to your engineering team prior to dispatch.
All brand-new components (FANUC, Siemens, Mitsubishi, Heidenhain, Renishaw, Fagor) carry a full 12-month factory warranty commencing from the date of bill of lading issuance. In the improbable event of an out-of-box electrical anomaly, our engineering team conducts immediate remote diagnostic analysis via video link. Should hardware failure be confirmed, we expedite replacement units under fast-track RMA procedures to prevent prolonged downtime on your Salto factory floor.
Absolutely. Consolidating orders is one of DingYan’s greatest cost-saving benefits for overseas manufacturing groups. You can combine FANUC pulse coders, Siemens synchronous motors, Renishaw workpiece styli, Mitsubishi drives, and Heidenhain handwheels into a single air-freight crate and unified commercial invoice. This dramatically lowers the fixed customs clearing fees, terminal handling costs, and inland courier tariffs imposed at São Paulo airports.
Alarm 414 is a composite error indicating an axis servo circuit defect. Our technical support protocol recommends checking the diagnostic display parameter No. 200/204 on your FANUC controller to identify the exact sub-bit (e.g., bit 5 for OVC overcurrent, bit 6 for LV low voltage, or bit 7 for HCA abnormal current). If the HCA bit is tripped, the IPM power module within the servo amplifier is likely punctured or the motor power cable has developed a ground fault. Contact DingYan with your diagnostic bit readout, and we will pinpoint whether the failure lies within the amplifier module or the motor winding.
Partner directly with Ningbo DingYan Machinery. Obtain guaranteed OEM components, expedited air logistics across São Paulo state, and 24/7 technical engineering verification from industry veterans.