Top-tier linear scales, power modules, and servo systems engineered for Serbian machine tool integrators and precision metalworking plants.
The manufacturing landscape of Serbia is undergoing a profound structural transformation. Centered in key industrial hubs such as Kragujevac, Novi Sad, Belgrade, Niš, and Subotica, Serbian industrial enterprises are expanding rapidly into high-precision automotive component production, heavy machine tool rebuilding, aerospace component tooling, and specialized agricultural machinery manufacturing. As tier-1 suppliers across Vojvodina and Central Serbia integrate deeper into the European Union supply chain, the demand for absolute positioning accuracy, thermal drift compensation, and micron-level repeatability has reached an all-time peak.
In traditional open-loop or semi-closed-loop CNC configurations—where position feedback is derived solely from rotary encoders attached to servo motor shafts—errors induced by ball screw thermal expansion, pitch backlash, lead deviation, and mechanical wear significantly impair final workpiece quality. In Serbian machining environments, where ambient shop-floor temperatures can vary dynamically between summer and winter, closed-loop direct linear measurement using Fagor Grating Rulers (Linear Optical and Magnetic Encoders) is no longer an optional upgrade; it is the fundamental prerequisite for achieving compliance with stringent ISO 9001, IATF 16949, and DIN quality metrics.
Engineering Key Note: Fagor Automation's proprietary optical reading technology eliminates backlash error entirely by taking physical measurements directly on the machine tool slide rather than calculating movement through mechanical drive components.
To understand why Fagor Grating Rulers are specified by major European machine tool builders and Serbian CNC retrofitting specialists, engineers must evaluate the physics of position measurement under heavy metal-cutting loads.
| Feedback Metrology Criteria | Indirect Measurement (Rotary Encoder + Ball Screw) | Direct Linear Measurement (Fagor Optical Glass Ruler) | Direct Long-Scale Measurement (Fagor Steel Tape Ruler) |
|---|---|---|---|
| Thermal Expansion Compensation | Poor (Ball screw thermal growth causes up to 40 μm/m drift) | Excellent (Glass substrate expansion coefficient matches steel structure) | Outstanding (Steel tape anchored to bed base absorbs machine expansion) |
| Mechanical Backlash Isolation | None (Backlash in bearings, couplings, and nuts affects position reading) | Complete (Reads true physical table location independent of drive train) | Complete (Direct reading on long-travel gantries up to 60 meters) |
| Resolution & Signal Fidelity | Calculated (Interpolated via rotary motor counts) | Sub-micron (Direct optical reading down to 0.01 μm / 10 nm) | High Precision (Digital output down to 0.1 μm) |
| Vibration & Contamination Immunity | High (Housed inside motor shell) | High (TDMS double sealing lips + IP67 pressurized air inlet) | Very High (Resistant to harsh chips and cutting oils in heavy machining) |
| Primary Serbian Industry Application | Basic Lathes & Auxiliary Axes | 5-Axis CNC Machining Centers & Precision Grinding | Large Gantry Mills & Horizontal Boring Machines (BFT Series) |
Fagor Automation provides two major architectural families of grating rulers tailored to diverse mechanical envelope constraints and stroke lengths across Serbian industrial facilities:
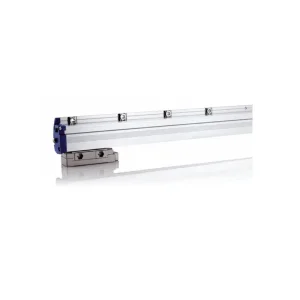
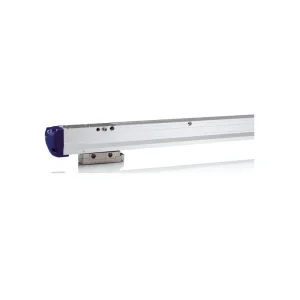
Designed for compact and medium-sized machine tools (measuring length from 140 mm up to 3,040 mm). Built upon a rigid aluminum extrusion profile containing a continuous optical glass scale etched with sub-micron line grids.
Engineered for large-span linear motion (measuring length up to 60 meters). Utilizes a flexible, high-accuracy stainless steel tape inserted into aluminum guide profiles.
Fagor's Thermal Displacement Management System ensures that the linear scale expands and contracts symmetrically from fixed anchor points, matching machine expansion curves.
Seamless protocol integration with global and regional controllers including Siemens SINUMERIK, FANUC, Mitsubishi, Heidenhain, and Fagor CNC systems.
Real-world integration of Fagor feedback metrology in Serbia's leading manufacturing clusters.
A major tier-1 automotive supplier in Kragujevac retrofitted three 5-axis vertical machining centers with Fagor G Series absolute grating rulers (EnDat 2.2 protocol). By switching from semi-closed-loop motor encoders to direct optical scale reading, the plant reduced thermal surface waviness on stamping dies by 78%, meeting strict OEM tolerances for European automotive body panels.
An industrial equipment rebuilder in Novi Sad upgraded a heavy horizontal boring machine using Fagor L Series continuous steel tape linear scales across X and Y axes (14m span). The modular steel tape design eliminated scale junction errors, allowing precision machining of massive gearbox casings for regional renewable energy projects.
A defense and high-precision hydraulics shop in Belgrade integrated Fagor nanometric optical rulers onto ultra-precision surface grinders. Housed within pressurized air-purged housings (IP67), the encoders maintained sub-micron repeatability despite continuous immersion in aggressive synthetic coolants.
As machine tool automation advances toward Industry 4.0 standards, linear optical feedback systems are evolving beyond passive positioning sensors into intelligent diagnostic devices. The next generation of Fagor grating rulers incorporates smart optical scanning heads equipped with embedded microprocessors, enabling real-time condition monitoring and predictive maintenance data exchange over industrial Ethernet backbones.
Real-time measurement of optical signal attenuation allows the CNC controller to alert operators to clean the scale long before position signal loss or machine emergency stopping occurs.
Thermal expansion coefficient sensors embedded directly inside the ruler housing feed dynamic deflection data to machine tool digital twins for micro-second thermal modeling.
Dual and quadruple reading head configurations on a single optical track enable simultaneous position measurement and mechanical pitch/yaw error dynamic self-compensation.
Sub-nanometer interpolation electronics combined with high-frequency signal processing support ultra-smooth feedrates on high-speed direct-drive linear motor axes.
Implementing closed-loop linear feedback onto existing machine tools in Serbia requires a rigorous engineering workflow to ensure mechanical alignment tolerances and electrical noise immunity are strictly maintained.
Prior to scale mounting, engineers measure machine way parallelism and mounting surface flatnesses using precision dial indicators or laser interferometers. Mechanical mounting surface parallelism must be within ±0.005 mm per meter to prevent reading head flexure.
The extruded aluminum body is secured to the machine bed using flexible mounting brackets that permit differential thermal expansion. Clean, oil-free dry compressed air (0.2–0.3 bar pressure) is connected to the scale body inlets to maintain positive internal air pressure against coolant spray.
Feedback cables are routed away from high-voltage AC spindle lines and servo motor power leads. Shielding continuity is verified to prevent electromagnetic interference (EMI) induced by shop-floor power electronics or heavy welding equipment.
CNC control parameters (such as FANUC axis parameter 2020/2084 or Siemens machine data MD31000/MD31020) are updated to recognize direct scale signal resolution. Proportional-Integral-Derivative (PID) position loops are tuned to eliminate mechanical resonance.
Original OEM components stocked for immediate air-express delivery to Serbian manufacturing facilities and service engineering units.
In-depth responses curated by our application engineers for maintenance professionals and buyers in Serbia.
