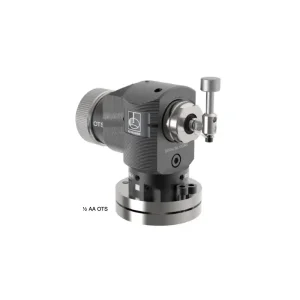
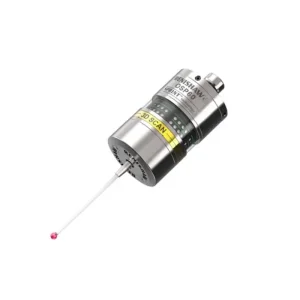
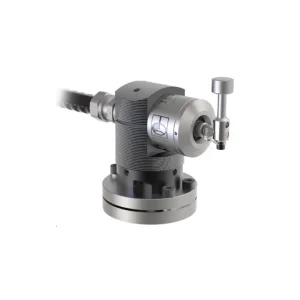
High-demand metrology probes, tool setters, and CNC controller spares ready for immediate deployment to Indianapolis facilities.
The Metropolitan Statistical Area (MSA) of Indianapolis, Indiana represents one of North America's most concentrated centers for high-precision manufacturing, advanced automotive powertrain engineering, aerospace component fabrication, and medical device machining. As machining tolerances shrink to the single-micron level, local production facilities require reliable access to precision measurement systems and OEM-level replacement components.
Renishaw precision probing hardware—spanning high-accuracy contact tool setters (such as the TS27R and OTS series), sub-micron optical probes (OSP60, RMP60), and specialized M2/M4 tungsten steel datuming styli—serves as the backbone of closed-loop quality control in modern machine shops across Marion, Hendricks, and Johnson counties. However, maintaining uncompromised operational efficiency requires more than acquiring physical hardware; it demands a robust supply chain, verified part compatibility, and localized technical expertise capable of resolving unplanned machine downtime instantaneously.
This comprehensive technical whitepaper examines the integration of Renishaw metrology spare parts within the Indianapolis industrial sector. It evaluates the regional market drivers, closed-loop CNC controller architecture (covering FANUC, SIEMENS, MITSUBISHI, and DELTA integrations), technical maintenance roadmaps, and international procurement protocols necessary to guarantee continuous, zero-defect manufacturing operations.
Advanced strain-gauge and mechanical contact touch-probes ensure consistent tool offset verification and part datum alignment across multi-axis milling centers.
Direct logistics coupling between regional staging hubs and Indianapolis International Airport (IND) freight zones minimizes emergency line-stop durations.
Every stylus, optical interface module, and CNC drive card undergoes strict signal verification and dimensional calibration prior to dispatch.
Known historically as the "Crossroads of America," Indianapolis has evolved into an advanced manufacturing stronghold. The region's economy relies heavily on automated production ecosystems requiring minimal human intervention and maximum machine uptime. Key sectors driving the demand for high-end Renishaw probing systems and CNC spare parts include:
When a probe stem snaps during a high-speed tool measurement cycle or an optical transmission module suffers thermal degradation, machine operations halt immediately. The cost of an idle 5-axis CNC machine in an Indianapolis job shop can exceed $500 per hour. Securing a reliable supply chain for original Renishaw probes, styli extensions, and matching CNC servo drives is essential to maintaining regional competitiveness.
To understand why proper part selection is critical, maintenance engineers must evaluate the mechanical and electrical principles governing Renishaw hardware. Renishaw touch-trigger probes operate on a patented kinematic resistive-grid seating mechanism. Three equally spaced rods rest on six tungsten carbide balls, forming an electrical circuit.
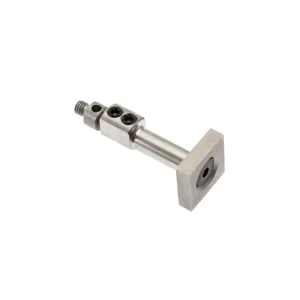
The choice of stylus stem material directly impacts measuring accuracy and deflection characteristics. For short, rigid styli, stainless steel stems are sufficient. However, for applications exceeding 30 mm in length—such as the Renishaw M4 Tungsten Steel Tool Datuming Cube Stylus (34.5 mm), A-2197-0160—tungsten carbide stems provide exceptional stiffness, minimizing stem bending during contact trigger cycles.
| Stylus Stem Material | Young's Modulus (GPa) | Thermal Expansion Coeff. | Primary Industrial Application |
|---|---|---|---|
| Tungsten Carbide | 530–700 | 4.5 × 10⁻⁶ /°C | High-rigidity tool setting cubes, long styli extensions, heavy shop floor use. |
| Ruby (Ball Tip) | 380–420 | 5.4 × 10⁻⁶ /°C | Standard spherical measuring tips; extreme hardness & wear resistance. |
| Carbon Fiber | 450 | -0.4 × 10⁻⁶ /°C | Ultra-lightweight extensions for long-reach deep bore probing. |
| Silicon Nitride | 320 | 3.2 × 10⁻⁶ /°C | Scanning aluminum alloys; resists material pickup (adhesion). |
Modern machine tools in Indianapolis auto plants employ two primary signal transmission technologies to connect the probe to the CNC interface:
Automated length and diameter measurement of cutting tools is essential for maintaining unattended lights-out production. The hardwired Renishaw TS27R uses a standard 4-wire interface linked to the machine skip input circuit. In contrast, the wireless Renishaw OTS uses optical infrared transmission, eliminating signal cables inside the work envelope to streamline installation on rotary table 5-axis machines.
A probe is only as effective as its integration with the host CNC controller. Precision component suppliers servicing Indianapolis must maintain inventory not only for Renishaw hardware, but also for matching CNC servo amplifiers, controllers, power supply modules, and high-resolution encoders.
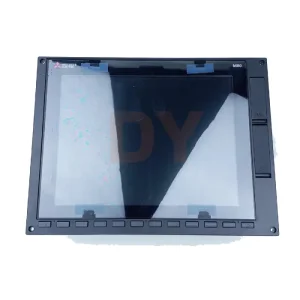
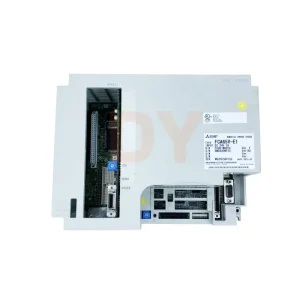
Integrations involving the Mitsubishi M80 Series (FCA80H-4B) and FCA65V-E1 NC Controllers require high-speed skip inputs via dedicated bus channels. Paired with OSA405S5AS absolute encoders and MDSC1V2-0505-N servo drive units, these systems process skip signals in under 1 millisecond, enabling precise high-speed probing without overtravel damage.
FANUC αi/βi series drives (such as the A06B-6200-H037 Servo Amplifier) and SIEMENS SIMOTICS 1FK7 HD Synchronous Servo Motors rely on rapid closed-loop position feedback. When a Renishaw probe triggers, the CNC latch circuit freezes axis coordinates instantly, executing automated macro updates (e.g., FANUC G31 / Siemens MEAS command).
As Industry 4.0 standards transform Midwestern manufacturing plants, in-process metrology is evolving from a reactive quality control check into a predictive, real-time process optimizer.
| Phase Level | Metrology Milestone | Hardware Requirement | Process Outcome |
|---|---|---|---|
| Phase 1: Basic Datuming | Manual edge finding replaced by automated 3D touch probing. | Renishaw TS27R or OTS Tool Setter + M4 Stylus. | Elimination of operator error; 70% faster fixture setup. |
| Phase 2: In-Process Control | Mid-cycle part feature verification and tool wear adjustment. | Renishaw OSP60 Scanning Probe + High-Speed Skip Interface. | Dynamic tool offset adjustments; continuous thermal drift correction. |
| Phase 3: Autonomous Manufacturing | Fully integrated lights-out cell with automatic part rejection and adaptive machining. | Renishaw RMP60 / Radio Receivers + Multi-Axis CNC Feedback (Mitsubishi M80 / Fanuc αi). | Zero scrap rates; complete closed-loop manufacturing for aerospace and medical components. |
Securing critical Renishaw spare parts in Indianapolis requires a resilient global supply chain. Precision items such as ceramic break-stems, styli datuming cubes, scanning modules, and CNC control components demand specialized storage, anti-static handling, and climate-controlled transport.
All probing components comply with international standards, including ISO 10360-2 for CMM and CNC touch probes. Replacement ruby spheres and tungsten carbide cubes are provided with certificate validation to support AS9100 Rev D aerospace audits across Indiana.
Through streamlined air freight routes linking major manufacturing warehouses directly to Indianapolis International Airport (IND), emergency orders bypass standard customs bottlenecks, enabling rapid delivery to local job shops.
Browse our verified stock of motors, amplifiers, encoders, and Renishaw probing parts supported with a 12-month quality warranty.
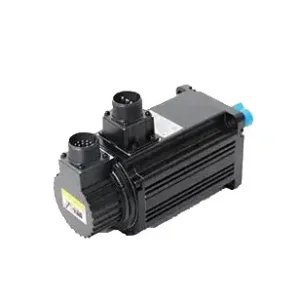
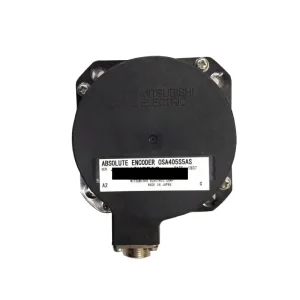
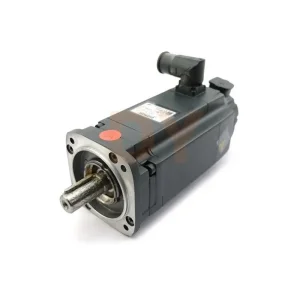
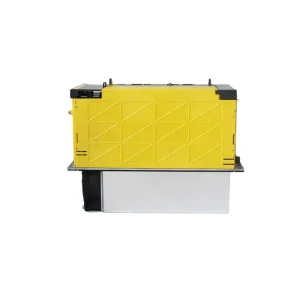
Key insights for machine shop managers, maintenance technicians, and procurement managers in Indianapolis.
Whether you require a replacement Renishaw M4 stylus cube, a hardwired TS27R tool setter, or a Mitsubishi/Fanuc servo drive, our application engineering team is ready to assist you 24/7.
Send Inquiry Now