Explore top-tier CNC hardware, precision encoders, servo amplifiers, and measurement solutions from verified global supplier inventories.
An in-depth engineering assessment of electromagnetic design, thermal management, and precision feedback integration in the CTB S18 Spindle Servo Platform.
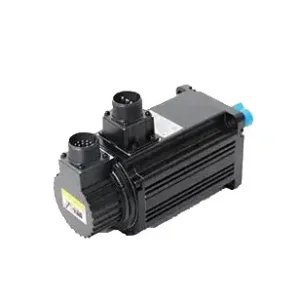
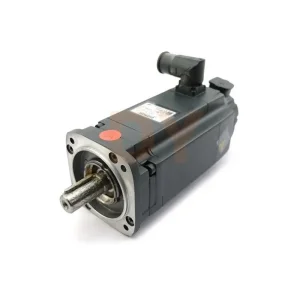
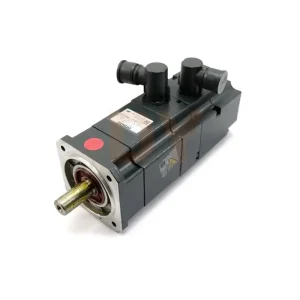
The CTB Servo Motor S18 series represents a flagship achievement in AC synchronous permanent magnet and induction spindle technology. Engineered by Beijing CTB Servo Co., Ltd., the S18 frame is optimized for high-power, high-torque spindle applications requiring dynamic response across wide speed ranges.
Featuring ultra-high density rotor lamination structures and N38UH high-temperature resistant NdFeB permanent magnets, the S18 maintains exceptional field stability even under severe duty cycles. Its low cogging torque design (<0.5% of rated torque) guarantees smooth low-speed interpolation required for complex 5-axis CNC machining, contouring, and thread cutting.
Thermal dissipation is critical to maintaining continuous output ratings without thermal growth affecting spindle accuracy. The CTB S18 incorporates dual-circuit cooling configurations: high-velocity forced air cooling (IP54/IP55) for standard turning centers, and closed-loop liquid cooling jackets (IP67) for ultra-precision grinding and heavy milling applications.
Embedded Class H insulation (180°C limit) combined with multi-point PT100/KTY84 thermistor sensors ensures real-time temperature feedback to the servo drive, protecting the motor against phase-to-phase thermal overloads while maximizing sustained power capacity.
Precise angular velocity and positional feedback are achieved through modular encoder interfaces. The S18 platform supports 23-bit multi-turn absolute optical encoders, 17-bit magnetic encoders, and high-frequency SinCos resolvers.
This versatile feedback architecture enables rigid tapping speeds up to 6,000 RPM, sub-arcsecond positioning accuracy for C-axis indexing on CNC turning centers, and seamless synchronization with global drive protocols including CTB GS series, Fanuc, Siemens SINAMICS, and Mitsubishi MDS platforms.
| Performance Specification | CTB S18 Servo Spindle Motor | Standard Induction Spindle Motor | Conventional AC Servo Motor |
|---|---|---|---|
| Rated Power Density | High (up to 1.8 kW/kg) | Low (0.6 - 0.9 kW/kg) | Moderate (1.1 - 1.3 kW/kg) |
| Low-Speed Torque Output | Full Rated Torque at 0 RPM (Constant Torque) | Weak low-speed torque drop-off | High torque, limited maximum RPM |
| C-Axis Indexing Accuracy | ±1.2 Arc-seconds (with 23-bit Encoder) | Not Suitable / Poor Control | ±5.0 Arc-seconds |
| Rigid Tapping Acceleration | 0 to 3000 RPM in < 0.15 sec | 0 to 3000 RPM in > 0.8 sec | 0 to 3000 RPM in 0.25 sec |
| Energy Efficiency Grade | IE4 / IE5 Ultra-Premium Efficiency | IE2 Standard Efficiency | IE3 Premium Efficiency |
How global machine tool integrators deploy the CTB S18 across diverse industrial environments to unlock machining performance and productivity.
In heavy manufacturing environments across Southern China and Eastern Europe, CNC lathes require immense torque at low RPM for rough turning of forged steel and alloy shafts, combined with rapid acceleration for secondary operations.
Implementation Reality: Equipping lathe spindles with the CTB S18 delivers constant high torque from 0 to 1,500 RPM, transitioning smoothly into constant power up to 8,000 RPM. This eliminates the need for mechanical gearbox speed reduction, significantly decreasing gear noise, maintenance overhead, and thermal growth.
Aerospace component manufacturing demands continuous high-speed end milling of aluminum alloys and titanium structures where tool chatter must be minimized.
Implementation Reality: Dynamically balanced to G1.0 standards, the liquid-cooled CTB S18 spindle motor runs at speeds up to 15,000 RPM with vibration velocities below 0.5 mm/s. Integrated real-time temperature tracking prevents spindle displacement, enabling micro-tolerance machining on complex curved surfaces.
Automated automotive production lines rely on direct-drive indexing tables for rapid workpiece positioning between robotic welding cells.
Implementation Reality: Leveraging the S18's 300% peak torque overload capacity and 23-bit optical absolute encoder feedback, indexing tables complete 90-degree rotations in under 0.18 seconds with zero backlash, accelerating line cycle times for tier-1 automotive component suppliers.
Flexographic printing and paper slitters require perfectly synchronized multi-axis shaft motion under dynamic load variations to avoid material tearing.
Implementation Reality: Operating on EtherCAT or CANopen fieldbus architectures, multiple CTB S18 motors execute real-time velocity synchronization down to sub-millisecond response windows, ensuring consistent material tension and zero print misalignment during high-speed runs.
Analyzing the shift toward energy-efficient, high-torque spindle motors in global industrial machinery retrofitting and new machine tool manufacturing.
Global machine tool manufacturers in Europe, North America, and East Asia are under increasing competitive pressure to deliver higher machining speed and accuracy while reducing total bill-of-materials (BOM) costs.
The CTB Servo Motor S18 offers machine builders a plug-and-play servo spindle alternative to legacy European brands at a competitive cost profile. Standard flange dimensions (DIN/NEMA compliance) and universal encoder interfaces simplify mechanical and electrical integration into new CNC lathe and milling platforms.
With thousands of legacy CNC machines operating globally, maintenance, repair, and operations (MRO) teams face rising costs when sourcing obsolete OEM spindle motors.
The CTB S18 has become a preferred retrofit component for upgrading aged asynchronous spindle motors. Replacing older induction drives with the S18 reduces overall machine power consumption by 22–35%, introduces C-axis contouring capability, and eliminates mechanical gearbox failures.
Factory operators evaluating life-cycle expenditures prioritize energy efficiency, reliability, and spare part availability.
By adhering to IE4/IE5 ultra-premium efficiency standards, an S18 operating 24/7 in an automated cell pays for its initial procurement cost within 14 to 18 months in energy savings alone. Coupled with low MTBF (Mean Time Between Failures) exceeding 30,000 hours, overall operational downtime is drastically curtailed.
Unlocking strategic cost advantages, rapid prototyping, and robust raw material security through Beijing and Yangtze River Delta industrial clusters.
The performance of permanent magnet AC servo motors hinges directly on raw material purity and magnet supply security. China processes over 80% of the world's NdFeB (Neodymium Iron Boron) rare-earth magnets.
CTB leverages direct domestic supply integration for high-grade N38UH and N42SH magnets. This guarantees structural immunity against demagnetization at temperatures up to 180°C while shielding international buyers from global material price volatility and supply bottlenecks.
CTB's manufacturing facilities feature automated slot-filling stator winding machines, vacuum pressure impregnation (VPI) insulation lines, and robotic rotor balancing rigs.
Automated coil winding increases slot fill factor to over 78%, maximizing copper utilization and reducing internal thermal resistance. Every CTB S18 motor undergoes 100% automated end-of-line testing, including hi-pot dielectric tests, back-EMF verification, and full-load burn-in trials.
Strategically connected with coastal shipping hubs like Ningbo and Shanghai ports, standard CTB S18 units can be dispatched within short lead times.
Furthermore, flexible manufacturing lines allow rapid OEM customization: special shaft keyways, custom front flange mounting dimensions, dual-shaft extensions, brake options, and tailored encoder output pinouts can be produced and shipped within weeks rather than months.
Anticipating next-generation advancements in wide-bandgap power semiconductors, AI diagnostic algorithms, and energy recovery.
The evolution of drive electronics is shifting from conventional IGBT modules to Silicon Carbide (SiC) MOSFET inverters. Next-generation iterations of the CTB S18 drive system will operate at carrier frequencies exceeding 32 kHz.
Higher switching frequencies eliminate audible motor noise, reduce current harmonics, and lower rotor eddy-current losses, resulting in cooler motor operation and extended bearing life.
Future CTB S18 hardware revisions integrate embedded MEMS vibration sensors and smart memory chips directly inside the motor housing.
Operating via MQTT or OPC UA protocols, the motor streams real-time health data—including bearing degradation frequencies, thermal trends, and winding resistance shifts—to cloud monitoring systems. Machine operators receive automated predictive maintenance alerts weeks before a potential bearing failure occurs.
In high-cycle machining operations featuring constant acceleration and deceleration, energy dissipation via braking resistors represents significant power waste.
The ongoing roadmap couples CTB S18 spindle motors with active front-end (AFE) regenerative drives. Kinetic energy during spindle braking is inverted back into pure AC line power or stored in common DC bus capacitor banks, reducing total machine hall power consumption by up to 28%.
Rigorous international certification frameworks, cross-brand replacement guidelines, and dedicated engineer support networks.
Every CTB Servo Motor S18 is manufactured under strict quality control standards audited to ISO 9001:2015. The platform carries full CE Certification under Low Voltage Directive (2014/35/EU) and EMC Directive (2014/30/EU).
Units built for North American export feature UL/cUL Recognized insulation systems, meeting NFPA 79 electrical safety standards for industrial machinery. All components comply with RoHS 3 and REACH environmental mandates.
Overseas buyers benefit from comprehensive engineering support provided by specialized industrial export partners. Before dispatches are authorized, engineers cross-reference motor nameplate data, shaft drawings, flange dimensions, and encoder protocols.
Detailed wiring diagrams, parameter parameterization files for Fanuc/Siemens/Mitsubishi controllers, and step-by-step installation manuals are provided to guarantee smooth commissioning without field trial errors.
All CTB S18 motors ship with a standardized 12-Month Factory Warranty covering electrical and mechanical failures under normal operating parameters.
In the event of an operational fault, fast-response remote telemetry analysis of alarm codes isolates whether the root cause stems from parameter misconfiguration, external short-circuits, or internal component wear, ensuring fast parts dispatch or local technical service resolution.
Common engineering questions regarding CTB S18 selection, drive compatibility, encoder matching, and retrofit procedures.
Complete your machine tool build or retrofit with authentic high-precision control modules and measurement units.