Direct supply of genuine high-accuracy contact tool setting systems engineered for harsh shop floor environments, severe thermal fluctuations, and heavy CNC milling operations.
In high-precision machining sectors across Russia—from the Urals heavy machinery clusters to St. Petersburg turbine plants—unplanned downtime and off-spec machining are major margin destroyers. Integrating robust Renishaw contact tool setters eliminates manual gauge errors and delivers verifiable ROI.
Modern metal-cutting facilities serving the Russian industrial sector face unprecedented demands for dimensional accuracy, rapid order execution, and operational independence. Manual tool height setting using slip gauges or eye-ball optical tools introduces severe human error, taking anywhere from 5 to 15 minutes per tool changeover. Over a standard multi-shift operation, this traditional approach accounts for dozens of non-productive hours every month per CNC machine tool.
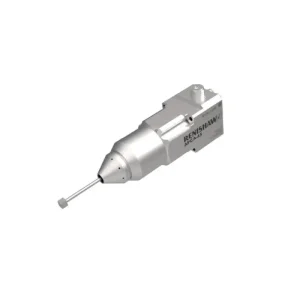
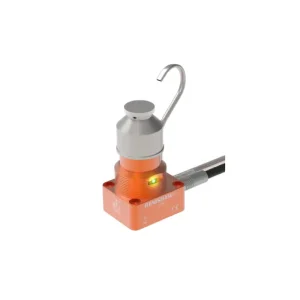
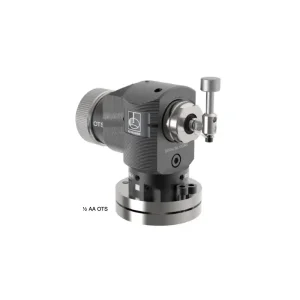
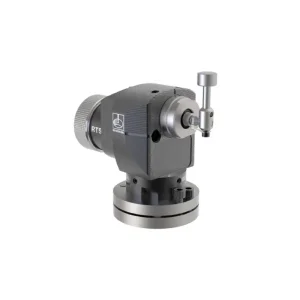
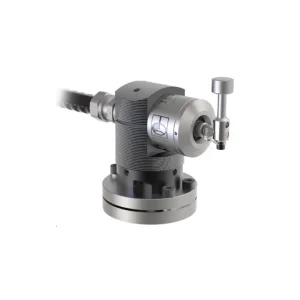
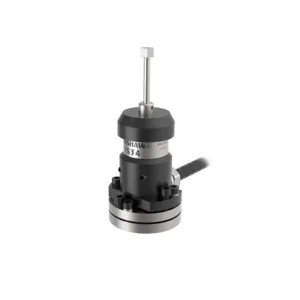
Renishaw contact tool setters—including world-renowned models such as the TS27R, TS34, RTS, OTS, LTS, and pneumatic APC/APCA/APCS series—solve this bottleneck by introducing automated in-process kinematic touch technology directly onto the CNC table. By measuring tool length, tool diameter, and checking for tool breakage prior to and immediately after critical cutting passes, these systems ensure closed-loop process stability even when operating under severe thermal drift.
The Russian manufacturing sector is undergoing a structural transition toward autonomous production and supply chain self-reliance. Major industrial hubs—such as Yekaterinburg, Chelyabinsk, Nizhny Novgorod, Samara, and Novosibirsk—are heavily investing in re-tooling existing machine fleets and expanding CNC machining capacity. Sub-sectors including heavy machinery manufacturing, energy generation equipment (turbines, pumps, valves), railway gear manufacturing, and aerospace component machining demand micron-level geometric accuracy.
However, ambient operating conditions in many Russian regional facilities present distinct challenges. Winter shop floor temperature swings, variable coolant quality, and continuous heavy-duty metal removal mean machine spindles experience continuous axial thermal expansion. Without automatic tool compensation, thermal expansion directly compromises workpiece tolerances, leading to costly scrap or rework.
Technical Insight: Axial thermal drift of a CNC spindle can exceed 30 to 50 micrometers during continuous high-RPM roughing operations. Implementing closed-loop Renishaw tool measurement cycles directly into machine G-code (via macros) offsets thermal drift in real time, guaranteeing consistent surface finishing and thread depth accuracy.
At the core of Renishaw contact tool setters lies the proven three-point kinematic spring-loaded contact mechanism. When the cutting tool stylus strikes the stylus disk, the internal mechanical contacts pivot, instantly interrupting an electrical circuit to trigger an ultra-fast skip signal back to the CNC controller (e.g., FANUC, SIEMENS SINUMERIK, Mitsubishi, or Balt-System).
Depending on the machine envelope and rotary table configuration, several transmission technologies are utilized across Russian factories:
Global procurement directors and Russian plant maintenance managers face a shared goal: eliminating supply chain risk while maintaining strict original-equipment quality standards. Substituting critical metrology components with non-verified third-party knock-offs frequently leads to signal jitter, pre-travel variance, and premature fluid ingress failure, resulting in catastrophic spindle crashes.
International buyers increasingly prioritize specialized partners who can provide verified genuine parts, deep cross-referencing capabilities (matching legacy part numbers with active production equivalents), and rapid export handling that eliminates administrative delays.
Situated in Ningbo, Zhejiang—one of China's premier industrial and logistics hubs—DingYan Machinery occupies a vital strategic position in the international industrial equipment supply chain. China's advanced Industry 4.0 manufacturing ecosystem allows direct access to tier-1 distribution channels, large-scale warehousing of original CNC components, and optimized quality assurance inspection pipelines.
Every Renishaw tool setter, FANUC drive, Siemens motor, and Mitsubishi encoder is guaranteed 100% new and original in factory sealed packaging. Comprehensive nameplate and serial documentation is provided prior to shipment.
Direct export capabilities from Ningbo port and international air express logistics (DHL, FedEx, express rail and direct freight routes to Russia) ensure critical spare parts arrive on time to mitigate unplanned shop floor downtime.
Experienced CNC control engineers verify part numbers, interface compatibility (e.g., HSI, MI 8-4), stylus lengths, and voltage parameters to ensure seamless plug-and-play installation upon arrival.
To demonstrate the practical impact of implementing automated contact tool setting, consider the following real-world application scenarios across major Russian manufacturing sectors:
Challenge: Excessive setup downtime when changing large-diameter face mills and modular boring bars on a heavy-duty floor-type horizontal boring mill.
Solution: Retrofitted a hardwired Renishaw TS27R contact tool setter with tungsten carbide stylus disk integrated directly into the FANUC 31i-B CNC system.
Results: Reduced tool measuring time from 18 minutes to 45 seconds per tool. Eliminated operator input errors, yielding a 99.4% first-pass yield on heavy steel gear housings.
Challenge: Micro-milling heat-resistant superalloys (Inconel 718) led to unpredictable tool wear and occasional micro-chipping during lights-out night shifts.
Solution: Installed an optical wireless Renishaw OTS tool setter paired with automated macro subroutines to measure tool radius and check for broken tools after every roughing cycle.
Results: Prevented spindle crashes caused by broken micro-endmills. Enabled continuous 24/7 un-monitored machining with zero scrapped blade forgings over a 12-month period.
Challenge: Heavy swarf accumulation and sticky high-viscosity oil coolant inside CNC turning centers frequently damaged fixed tool setting styli.
Solution: Deployed a pneumatic Renishaw APCA-45 tool setting arm that automatically extends into the cutting zone for tool measurement and retracts into a sealed protective housing during cutting operations.
Results: Protected the metrology hardware from chips and coolant blast, delivering over 50,000 flawless tool measurement cycles without mechanical failure.
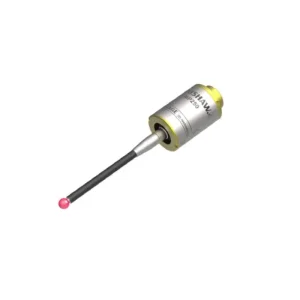
Complete single-source procurement for CNC tool setting hardware, workpiece inspection probes, FANUC spindle drives, Siemens servo motors, and Mitsubishi power conversion units serving the Russia market.
Detailed engineering answers regarding installation, signal interfacing, macro programming, logistics, and warranty terms for customers in Russia.
Get in touch with Ningbo DingYan Machinery's technical sales engineers today. Receive instant stock confirmation, price quotations, and verified part compatibility within 24 hours.
