A comprehensive examination of how integrated probing systems, automated tool setters, and direct china supply chain hubs eliminate scrap rates and unlock ultra-precision machining performance.
In modern high-speed CNC milling, turning, and multi-axis machining centers, maintaining dimensional tolerances within single-digit micrometers is no longer a luxury—it is an absolute prerequisite for Tier-1 automotive, aerospace, semiconductor, and medical device manufacturing. As global procurement officers and maintenance engineers search for a verified discount Renishaw CNC supplier, the underlying objective extends beyond basic unit price reduction. Procurement teams seek a reliable partner capable of delivering 100% genuine, high-precision industrial metrology hardware alongside technical field application knowledge, rapid export logistics, and comprehensive component warranty assurances.
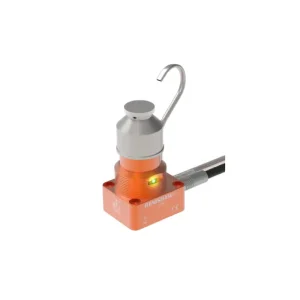
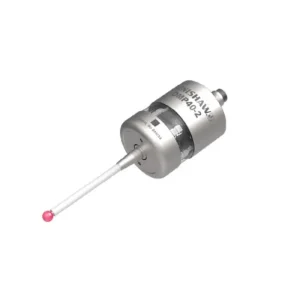
Renishaw probing systems—ranging from miniature optical workpiece inspection probes like the Renishaw OMP40-2 to robust hard-wired tool setting devices such as the Renishaw LTS and RTS contact tool setters—represent the global gold standard in closed-loop manufacturing feedback. By integrating real-time touch probing directly into the machine tool controller (whether FANUC, Siemens SINUMERIK, Mitsubishi M80, or Heidenhain), manufacturers convert offline inspection bottlenecks into automated, in-process quality control nodes. Partnering with a specialized China-based factory direct supplier allows global enterprises to optimize their Total Cost of Ownership (TCO) without sacrificing metrological integrity.
Search engines and industrial buyers do not simply seek catalog listings; they demand actionable technical depth. True supply chain resilience relies on understanding component interchangeability, signal transmission protocols (optical vs. radio vs. hard-wired), and parameter integration across multi-brand controllers including Siemens, Fanuc, Delta, and Mitsubishi.
Deconstructing kinematically restrained mechanisms, strain-gauge sensor physics, and optical transmission parameters.
Renishaw's classic 3-point kinematic design features three equally spaced rod-and-ball contacts. Upon physical deflection of the ruby stylus, the electrical resistance changes instantly, issuing a high-speed trigger signal to the machine tool spindle latch register with sub-micron repeatability.
Probes such as the Renishaw OMP40-2 utilize modulated infrared light transmission to communicate with the receiver (OMI-2T / OSI). Modulated transmission rejects optical noise from shop-floor LED lighting, arc welding, and neighboring machine optical sensors, guaranteeing zero false triggers.
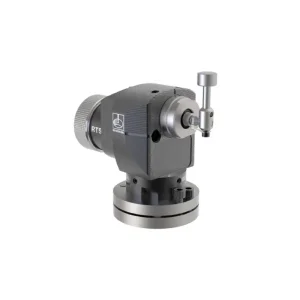
The LTS (Length Tool Setter) and RTS (Radio Tool Setter) break stylus contact to determine cutting edge length, tool radius, and tip breakage in real-time. This eliminates manual height gauge gauge-block errors, reducing tool offset setup time by up to 90%.
To assist procurement engineers in selecting the correct metrology hardware, the table below outlines core performance criteria across primary Renishaw touch probe and tool setting configurations available from stocked China suppliers.
| Model Series | Primary Application | Transmission Type | Unidirectional Repeatability | Enclosure Rating | Ideal Machine Type |
|---|---|---|---|---|---|
| Renishaw OMP40-2 | Workpiece Setup & Inspection | Modulated Optical (Infrared) | 1.0 μm (0.00004 in) | IPX8 (Hermetically Sealed) | Small-to-Medium 3/5-Axis Machining Centers |
| Renishaw LTS | Tool Length & Wear Setting | Hard-wired Cable (PNP/NPN) | 0.75 μm (0.00003 in) | IP68 Stainless Steel | Vertical Milling Centers & Tapping Centers |
| Renishaw RTS | Tool Length & Diameter Setting | 2.4 GHz Frequency Hopping Radio | 1.0 μm (0.00004 in) | IPX8 Chemical Resistant | Large Gantry Mills & Multi-Axis CNC Machines |
| Renishaw RMP60 | Complex Part Geometry Datuming | FHSS Radio Transmission | 1.0 μm (0.00004 in) | IPX8 Fully Submersible | 5-Axis Heavy Aerospace Machining |
Leveraging direct factory partnerships, localized inventory warehousing, and streamlined export mechanics for global CNC spare procurement.
The phrase "Discount Renishaw CNC Supplier" is frequently misunderstood by procurement professionals. In the context of Ningbo DingYan Machinery Co., Ltd., discount pricing does not mean refurbished or grey-market compromises. Instead, it reflects an optimized, high-volume supply chain framework centered in Ningbo, Zhejiang—one of the world's most sophisticated precision manufacturing and shipping hubs.
By consolidating bulk purchasing directly through official regional distribution channels, contract manufacturing partners, and factory-direct inventories, Chinese suppliers operate with dramatically lower overhead costs compared to Western regional distributors. These structural efficiencies translate directly into 15% to 35% cost savings for international clients needing genuine CNC hardware.
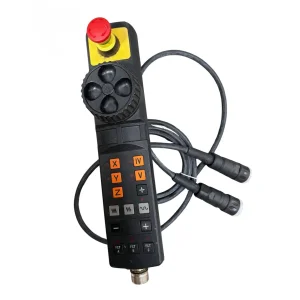
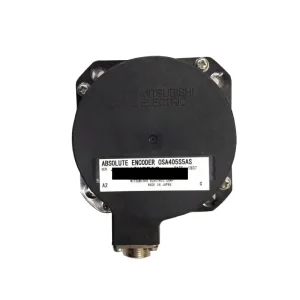
Over 10,000+ fast-moving CNC components are held on the shelf in Ningbo, including Renishaw probes, Fanuc servo amplifiers, Mitsubishi absolute encoders (OSA405S5AS), Siemens SIMOTICS motors, and Heidenhain HR410 handwheels.
Bypassing multi-tiered local sub-dealers allows direct factory pricing to be passed directly to global end-users, machine tool retrofitters, and maintenance facilities without middleman markups.
Direct integration with DHL, FedEx, UPS, and TNT express networks guarantees that critical machine-down replacement parts reach manufacturing plants across North America, Europe, and Southeast Asia within 3 to 5 business days.
Mitigating line-stop downtime, ensuring multi-brand system compatibility, and maintaining component traceability.
For enterprise procurement directors operating high-volume machine shops, an unplanned machine stoppage can cost anywhere from $500 to over $5,000 per hour in lost throughput. When a 5-axis machining center throws a probe optical error code, a servo drive alarm (such as Fanuc SV0401 or Mitsubishi MDS alarm), or an encoder feedback failure, speed of component delivery is as vital as pricing.
A holistic procurement strategy relies on multi-brand component availability. Facilities rarely run homogeneous machine fleets. A typical modern shop floor operates a mix of FANUC turning centers, Siemens 5-axis gantries, Mitsubishi high-speed die-mold centers, and Delta automated secondary operations. Purchasing from a unified supplier capable of shipping a Renishaw contact tool setter alongside a Siemens 6ES7 PLC CPU, a Heidenhain HR410 electronic handwheel, or a Fagor G-Series linear scale dramatically simplifies vendor management and cuts international freight overhead.
To eliminate expensive cross-border return cycles, expert China suppliers perform thorough pre-dispatch audits. Component order numbers, voltage tolerances, flange dimensions, firmware revisions, and nameplate photos are verified in writing against client electrical schematics prior to release.
How IoT-connected Renishaw touch probes and adaptive control loops are shaping autonomous manufacturing.
The manufacturing landscape is undergoing a rapid transition toward fully autonomous lights-out machining. In this paradigm, industrial touch probes and continuous tool setting devices are no longer optional alignment aids—they act as the vital sensory organs of the smart CNC factory. Modern industrial trends emphasize three core technological integrations:
As machine tool spindles heat up during multi-hour operations, ambient thermal expansion induces Z-axis growth. Renishaw tool setters automatically perform periodic thermal re-calibration cycles, updating macro variables dynamically without operator intervention.
Workpiece inspection probes calculate exact stock allowance on raw castings, updating 5-axis work coordinate systems (G54-G59 / WCS) on the fly. This prevents cutter damage caused by uneven forging allowances.
High-speed contact setters verify tool tip presence in under 1.5 seconds between tool changes. If a drill or end mill snaps, the controller immediately triggers a safe retract macro and calls a spare twin tool, preventing scrap production.
Examining how high-precision Renishaw hardware solves critical manufacturing challenges across specialized sectors.
Challenge: Excessive setup variation on complex 5-axis Inconel and Titanium turbine blades leading to tight wall thickness failures.
Solution: Implementation of the Renishaw OMP40-2 optical probe to perform multi-point surface alignment routines, establishing datum offsets directly within the Siemens SINUMERIK 840D controller.
Result: Scrap rates dropped to 0%, while part setup time fell from 45 minutes to 4.5 minutes.
Challenge: Frequent micro-breakage of small carbide drills leading to ruined cylinder block threads during high-speed 24/7 machining.
Solution: Installation of Renishaw LTS contact tool setters connected directly to Fanuc 0i-MF macro interrupt inputs.
Result: Immediate automated fault detection prevented damaged engine blocks, saving over $140,000 annually in scrap costs.
Challenge: Maintaining sub-micron cavity height consistency across 64-cavity injection mold plates using Mitsubishi CNC systems.
Solution: Combining Mitsubishi absolute encoders (OSA405S5AS) with Renishaw high-precision stylus systems to achieve ultra-fine tool offset compensation.
Result: Mirror-finish cavity depth variations were locked within ±0.8 micrometers across all mold positions.
Ensuring 100% component authenticity, operational reliability, and global regulatory compliance.
Purchasing precision electronics and optical metrology gear internationally requires robust compliance frameworks. Ningbo DingYan Machinery Co., Ltd. enforces strict Quality Assurance (QA) protocols to safeguard every shipment leaving our warehouse:
Authoritative answers from senior CNC application engineers regarding Renishaw hardware selection, controller compatibility, order verification, and international shipping.